- This topic is empty.
-
AuthorPosts
-
2026-11-05 at 5:13 pm #11114
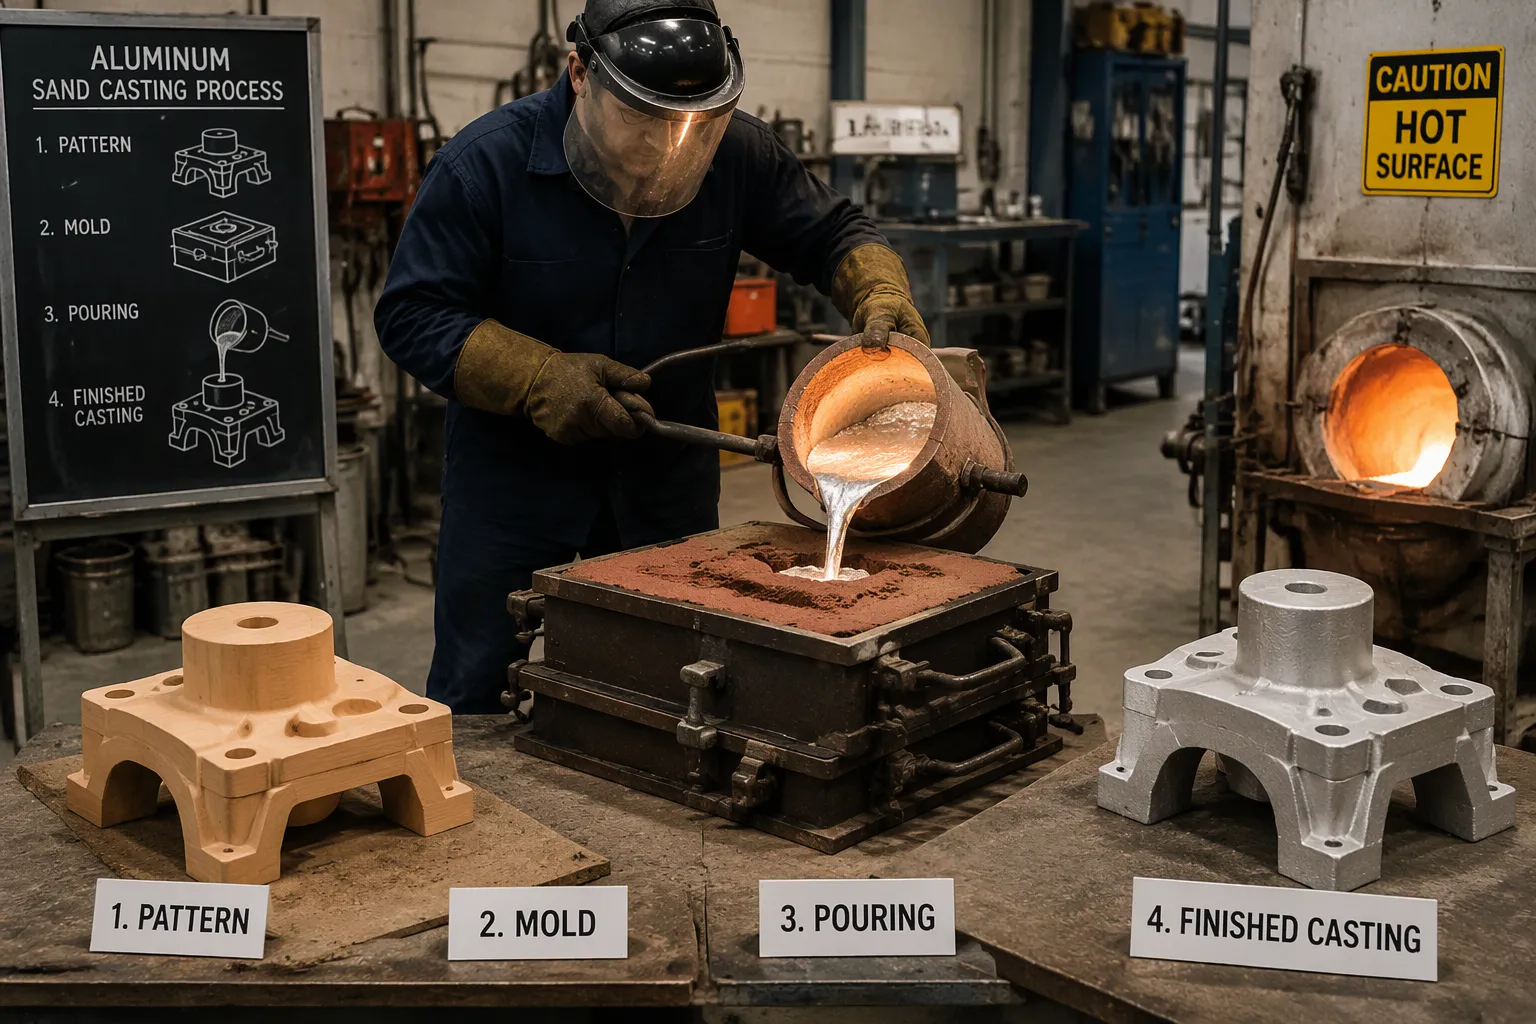
Image Source: https://www.xuxiangtaimetal.com Aluminum sand casting is a manufacturing process in which molten aluminum is poured into a sand mold formed around a pattern to create a finished part. As the most widely used casting method, it offers a cost-effective route to aluminum components with complex geometries. The process accommodates everything from simple prototypes to large, intricate parts, and it remains central to modern manufacturing. In practice, the workflow begins with pattern making and mold preparation, followed by melting and pouring the aluminum, then cooling, shakeout, and final cleaning and inspection. Each of these main steps of aluminum sand casting can be tailored to meet the dimensional and performance requirements of industrial applications.
Key Takeaways
- Aluminum sand casting is a low-cost way to make complex aluminum parts, from small prototypes to large industrial components.
- The process follows clear steps: pattern making, mold preparation, melting and pouring, cooling, shakeout, and finishing.
- Careful control at each step ensures high-quality castings and reduces defects.
What Aluminum Sand Casting Is and How the Process Works
A Definition in Plain Terms
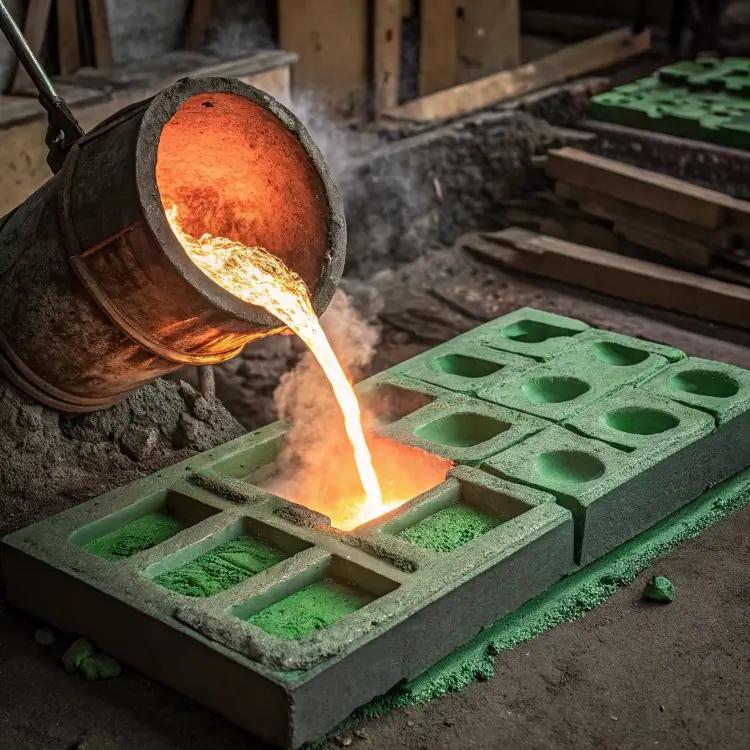
Aluminum sand casting is a process that pours molten aluminum into a mold cavity formed in sand. The MIT Center for Bits and Atoms describes sand casting in exactly these terms: molten metal flows into a cavity shaped in sand and then solidifies into the desired part. The sand is not a passive filler. It is the material that defines the outer shape of the casting, and in many setups it also defines internal passages and recesses.
A more detailed definition comes from the American Foundry Society’s Metalcasting Institute. Precision sand casting with aluminum alloys uses an assembly of resin-bonded sand cores to form the mold. Workers assemble these cores piece by piece, sometimes holding them in place with adhesives, fasteners, straps, or interlocking features. The complete assembly is called the core package. Instead of a steel mold forming the outer surfaces, the resin-bonded sand in the core package forms every surface of the part. The casting itself takes place when molten aluminum is poured or injected into that package.
This definition matters for anyone who writes a professional and informative B2B technical article about aluminum sand casting for industrial applications. The process is simple in concept and flexible in execution. A pattern establishes the geometry, sand packs around it, and molten aluminum takes the shape of the cavity. The same basic principle serves a one-off prototype and a production run of thousands of parts.
Why Sand Molds Are Used for Aluminum
Sand is the molding material in this process, and that choice brings several practical advantages. Boose Aluminum notes that sand casting is a relatively inexpensive molding process. It can create anything from small, detailed, intricate shapes to larger, simpler designs. The method begins with a sand mold shaped to the desired form. Molten metal fills the mold and solidifies into the final product.
Aluminum pairs well with sand for several reasons. The metal melts at a moderate temperature compared with ferrous alloys, so ordinary sand systems handle it without exotic refractory requirements. Molten aluminum also flows readily, which helps it fill thin sections and fine details in the cavity. Sand molds tolerate irregular curved surfaces and internal cavities without the need for complex steel tooling. A wooden or resin pattern can be modified at low cost when a design changes, and that flexibility keeps small-batch trials affordable.
Sand also allows a range of part sizes. A foundry can produce a compact bracket or a large housing on the same general equipment. The mold material is expendable, so each casting receives a fresh cavity. This feature supports design freedom, because the pattern can include features that would be difficult or impossible to machine. The process also accepts integrated machining allowances, which lets the foundry leave extra material where precision cuts will follow.
Where the Method Fits Among Casting Processes
Sand casting occupies a distinct position among casting processes. Die casting and investment casting each serve different needs, and the right choice depends on volume, tolerance, surface requirements, and part size. The comparison below draws on published guidance from Dixon Valve, Gabrian, Howard Precision, and MetalTek.
Attribute Sand Casting Die Casting Investment Casting Upfront cost Lower mold cost; wooden or resin patterns are inexpensive High tooling cost for steel dies Higher cost per part; mold is remade each cycle Production volume Fits low to medium runs and large parts Best for high-volume runs Fits low to medium volume projects Dimensional accuracy Lower than the other two methods; suited to parts without tight tolerances High accuracy and consistency Tight tolerances and excellent detail Surface finish Rougher, because compacted sand imprints its texture Very smooth finish from polished die walls Exceptional finish and fine detail Part size Excellent for large parts Typically small to medium parts Small to medium parts; larger than die casting allows Part complexity Handles complex shapes and internal cavities Preferred for thin walls and complex small parts Complex geometries and thin walls Best fit Fast turnaround, restrictive budget, or very large parts Complex, small-to-medium parts at high volume Precision parts in low to medium volumes Die casting excels when a program needs high volume, thin walls, and a smooth surface. Investment casting shines when precision and fine detail matter more than unit cost. Sand casting fits programs that need fast turnaround, a lower tooling budget, or very large parts. It also suits parts that do not require tight dimensional tolerances or extensive machining, according to MetalTek. Each process has a natural home, and many industrial programs use more than one.
The main steps of aluminum sand casting follow a logical sequence from pattern to finished part. Each step builds on the one before it, and each step offers control points for quality. The next section walks through that sequence in detail.
Main Steps of Aluminum Sand Casting
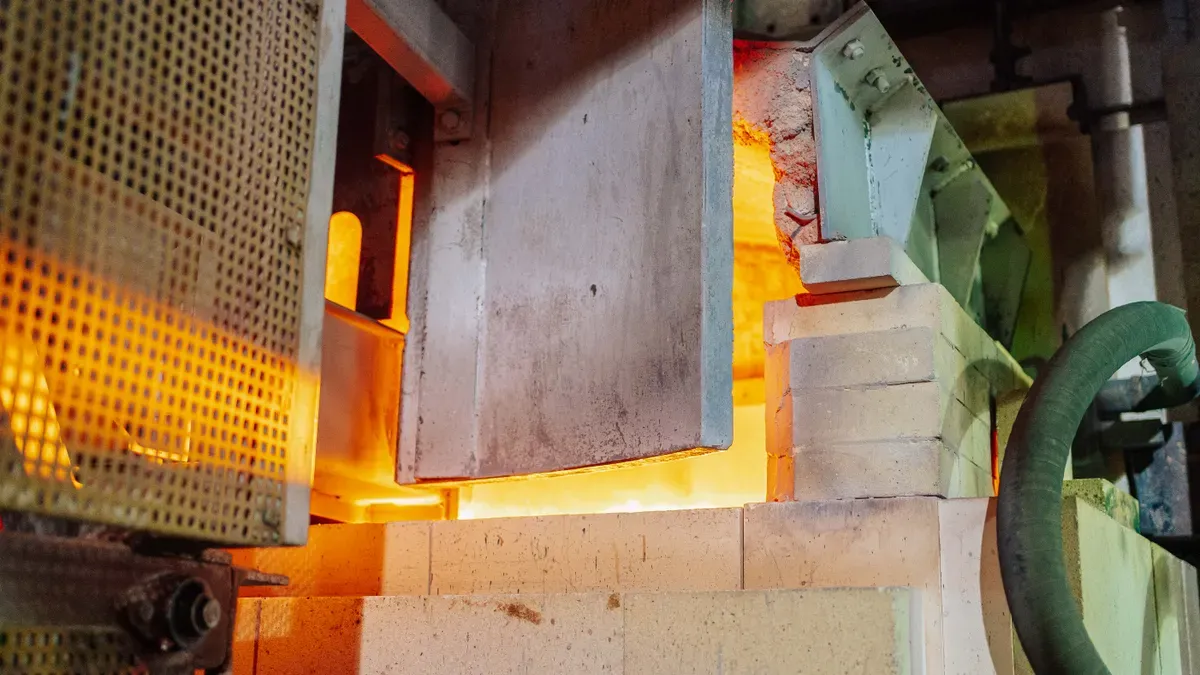
Image Source: https://www.xuxiangtaimetal.com The main steps of aluminum sand casting follow a fixed sequence. Each stage prepares the ground for the next one, and each stage carries its own quality controls. A defect introduced at the pattern stage will travel downstream. A pouring error will surface only after shakeout. Understanding the full chain helps buyers and engineers specify the right requirements at the right moment.
Pattern Creation
The pattern is the physical replica of the part. It defines the cavity that the sand will hold, and its dimensions include allowances for shrinkage, draft, and machining. Pattern quality sets the ceiling for casting accuracy. A worn or warped pattern will produce worn or warped parts, no matter how carefully the foundry handles the later steps.
Material choice for the pattern depends mainly on production volume. Rotocast Mold offers a practical guide based on annual piece counts.
Annual Volume Typical Pattern Material Up to ~50 pieces/year Wood 50–5,000 pieces/year Plastic / Polyurethane 5,000+ pieces/year Metal (aluminum or iron) The molding process also shapes the decision. Rotocast Mold notes that manual green sand and air-set processes work well with wood and polyurethane patterns. Automated green sand lines typically use aluminum matchplates and cope-and-drag patterns. High-pressure, vertically parted, and shell molding processes favor iron patterns.
Some geometries call for a different approach. Silicone rubber patterns are cast from a master and reproduce fine surface detail with enough flexibility to demold complex shapes cleanly. Smooth-On’s Mold Max XLS II, a low-shrinkage formulation used for sand casting patterns, reaches a Shore 30A hardness with 0.001 in/in shrinkage, 550 psi tensile strength, and 375% elongation. These properties suit geometries that would lock a rigid pattern in place. Silicone patterns fit short-run or specialty castings, parts with undercuts, and small-batch custom work. They are not intended for high-volume or automated production, where metal or high-density polyurethane offers better rigidity and wear resistance under sustained compaction forces.
Pattern design must also respect the parting line. A slight taper, called draft, on surfaces perpendicular to the parting line lets the pattern leave the sand without disturbing the cavity. The sprue and riser layout belongs in the pattern plan as well, because proper metal flow and gas escape depend on it.
Mold Making and Sand Packing
Mold making turns the pattern into a cavity that can accept liquid metal. The standard sequence for a two-part flask, as described by Wikipedia’s sand casting reference, runs as follows.
- Prepare a multi-part molding box (casting flask) with a top half (cope) and a bottom half (drag) to receive the pattern.
- Fill the lower portion of the box with molding sand, packed in through a vibratory process called ramming and periodically screeded level.
- Stabilize the sand surface with a sizing compound.
- Place the pattern on the sand, add another box segment, and ram additional sand over and around the pattern.
- Place a cover on the box, then turn and unlatch it so the halves part and the pattern, sprue, and vents can be removed.
- Add sizing, repair any defects from pattern removal, and close the box again.
The resulting “green” mold must be dried before it receives hot metal. Moisture left in the mold can trigger a steam explosion during pouring. Some shops oil the sand instead of moistening it, which removes the drying wait. Chemical binders such as furane resins or amine-hardened resins offer another route. With air-set or no-bake methods, the sand mixture is packed around the pattern, tamped down as it is added, and sometimes vibrated to compact the sand and fill voids. The pattern and any channel plug are then removed, leaving the cavity.
Sand selection is a technical decision in its own right. Wikipedia lists seven properties that matter.
- Refractoriness: the sand must withstand the liquid metal temperature without breaking down. Aluminum alloys need only about 650 °C (1,202 °F), far below the 1,500 °C (2,730 °F) that steel demands.
- Chemical inertness: the sand must not react with the metal.
- Permeability: the sand must vent gases produced during pouring. Each cubic centimeter of water added to the mold produces 1,600 cc of steam.
- Surface finish: finer particles give a better finish but reduce permeability.
- Cohesiveness: the sand must hold its shape after the pattern is removed.
- Flowability: the sand must fill intricate details and tight corners.
- Collapsibility: the sand must strip off the casting easily after solidification. Poor collapsibility can cause cracking and hot tears in metals that contract strongly during cooling.
A typical green sand mix contains silica, chromite, or zircon sand at 75 to 85%, bentonite clay at 5 to 11%, water at 2 to 4%, inert sludge at 3 to 5%, and anthracite at 0 to 1%. Green sand can be reused after the lost moisture and additives are replenished.
Defects that originate in the mold are well documented. Amfas International traces gas porosity to high sand moisture, poor venting, insufficient metal degassing, and turbulent flow. Shrinkage cavities trace back to weak riser design and missing directional solidification. Misruns and cold shuts come from low pouring temperature, slow pouring, thin walls, or poor gating. Swell and mismatch come from soft ramming, weak mold strength, improper flask alignment, or worn tooling. Each cause has a matching control: better compaction, precise alignment, consistent tooling maintenance, and disciplined sand quality checks.
Melting and Pouring
Melting brings the aluminum to a controlled liquid state. Matson Metallurgical recommends holding the melt above 705 °C for 40 to 60 minutes to eliminate gas and impurities. The pouring temperature then sits in the 720–750 °C range. The MIT Center for Bits and Atoms gives a comparable figure in Fahrenheit: a proper pouring temperature between 1,300 and 1,400 °F, with typical handling temperatures of 1,300–1,450 °F.
Pouring technique matters as much as temperature. Matson advises a slow, steady pour to avoid bubbles and inclusions. Watry Industries notes that a controlled pour reduces turbulence, air entrapment, oxide formation, and gas-related porosity. Tilt-pour and other automated pouring systems are common in advanced foundries for exactly this reason. Consistency across thousands of pours depends on repeatable motion, not operator feel.
Safety deserves explicit attention at this stage. The greatest danger is moisture. A single drop of water trapped under molten metal can cause a steam explosion, according to C-adtech. Tools and scrap must stay bone-dry, and molds and scrap should be preheated to drive off atmospheric moisture. The Recycled Materials Association reports that such explosions can throw molten aluminum up to 30 feet in all directions. At high temperature, aluminum also reacts with water to form aluminum oxide and release hydrogen, and the reaction is exothermic. Personal protective equipment includes a full face shield over safety glasses, leather welding gloves, cotton or wool clothing, and high-top leather boots. Respiratory protection is needed when melting coated scrap or using fluxes.
Cooling and Shakeout
After pouring, the casting solidifies inside the mold. Cooling rate influences the final microstructure, the distribution of shrinkage, and the residual stress state. Controlled cooling supports soundness. Rushing the cooling step can introduce thermal stress and cracking, and the LinkedIn casting community lists premature removal from the mold as one of the top causes of casting cracks. The same source recommends controlling mold cooling and casting removal timing as a practical prevention measure.
Shakeout frees the casting from its sand. Align Manufacturing describes the range of methods in use. In smaller foundries, workers lift the casting out with tongs as the mold crumbles. In larger operations, agitation or vibration tables shake unflasked molds so the sand detaches and falls through perforated surfaces into collection bins. The reclaimed sand can then be treated and reused. Precise Cast describes the same principle: the casting sits on a vibration table, the sand dislodges, and the loose sand drops into a box below for future casting.
Internal cores need their own removal step. Mechanical agitation, chemical treatment, or heat application can loosen the core, depending on the binder. Cores made with chemical binders may respond to solutions of sodium or potassium hydroxide. Steam, cold water, or other thermal treatments can weaken the core material. Once the core loosens, an agitation table or pneumatic hammers clear the remaining sand.
Finishing and Inspection
Finishing removes the traces of the casting process. Gates, runners, and risers are cut away. Flash and parting-line fins are ground flush. The surface may then receive sandblasting, pickling, passivation, mechanical polishing, or anodizing, depending on the drawing requirements. Machining allowances left at the pattern stage are consumed here, and CNC operations bring critical features to final tolerance.
Inspection verifies that the part meets its specification. Genfoundry describes a layered approach. Visual and dimensional inspection is the first defense. Visual checks target cracks, hot tears, scabs, fins, flash, wash-related surface issues, and burn-on or surface inclusions. Dimensional inspection must use the correct datums and measure the critical features defined by engineering. A part can pass a limited set of safe dimensions and still fail at core seating, mating faces, or locally controlled thickness features.
Internal quality needs methods beyond the surface. Radiography locates and characterizes internal porosity, shrinkage voids, and inclusion indicators. Metallography becomes valuable when results are borderline or a defect trend emerges. It characterizes microstructure and links it to solidification behavior, which helps distinguish gas-related porosity from shrinkage feeding limitations or oxide-related turbulence. Mechanical testing provides the final functional check. Depending on the alloy and application, this may include tensile testing, hardness, impact testing, and heat-treat condition checks.
A structured inspection flow ties these methods together. Dimensional inspection verifies geometry against defined datums and critical features. Surface inspection checks integrity where it affects machining, sealing, fatigue behavior, or assembly. Internal quality verification through nondestructive testing or metallography checks soundness that visual inspection cannot reveal. Mechanical testing then confirms performance, provided the coupons represent the relevant casting regions and section thicknesses.
Prevention supports inspection. Amfas International recommends optimized gating and riser design using simulation software, controlled pouring temperatures and solidification rates, strict sand quality and moisture control, clean melt practices with filtration, and in-process inspection backed by statistical process control. These measures reduce the defect population before the inspector ever sees the part.
A professional and informative B2B technical article about aluminum sand casting for industrial applications should treat these five stages as one connected system. Pattern accuracy, mold integrity, pour control, cooling discipline, and inspection depth all feed the same outcome. The main steps of aluminum sand casting reward attention at every link, and the main steps of aluminum sand casting leave little room for shortcuts.
Materials, Benefits, and Applications
Materials Used in Aluminum Sand Casting
Alloy selection shapes the mechanical properties, corrosion behavior, and machinability of a sand casting. WB Castings lists five alloys that cover most industrial needs.
Alloy Description 319 Great machining and casting characteristics; used for structural castings in automotive and transportation parts and other general commercial applications. A356 Improved mechanical properties such as strength, elongation, and ductility; primarily used in heat treatment applications and castings that need high strength. C355 Similar to A356 with added copper to improve strength at higher temperatures; best for pressure-tight applications. 535 High-strength aluminum that reaches full properties without heat treatment; offers great corrosion resistance, excellent machinability, and dimensional stability. 713 High-strength casting alloy that is not heat treated; great yield, elongation, and tensile properties, with the best impact strength achieved through natural aging. A380 remains a workhorse grade for structural and fluid-handling components. It offers high fluidity and good machinability, and it suits integrally formed parts with complex internal channels.
Key Advantages of the Process
The Foundry Group summarizes the core strengths of aluminum sand casting.
- Design versatility: custom parts of various shapes, sizes, and complexities with precision.
- Lightweight results: a high strength-to-weight ratio that reduces weight without compromising strength.
- High strength and durability: long-lasting performance under demanding conditions.
- Corrosion resistance: a natural oxide layer, with optional coatings for enhanced durability.
- Excellent appeal: a sleek, modern appearance for aesthetic products.
- Rapid production: faster processing than other metals, with shorter lead times.
- Cost-effectiveness: high quality at lower production and material costs.
- Recyclability: efficient recycling that requires less energy than virgin extraction.
Design versatility: Aluminum sand casting helps create intricate designs and complex shapes, allowing for more design flexibility. This is especially useful for creating custom parts and components. — Bremmer Manufacturing
Air-set molding extends this flexibility further. CM-Tec notes that chemically bonded sand accommodates larger castings, more intricate geometries, heavier sections, and complex core packages.
Suitability for High-Volume Production
Sand casting serves small to large production runs, according to Precision Enterprises. Boose Aluminum describes it as most cost-effective for low, medium, and occasionally high volumes, thanks to relatively low upfront tooling costs. Precise Cast places the practical threshold near 1,000 units per month. Above that level, die casting often becomes the lower-cost route. Kinetic Diecasting calculates a break-even point of roughly 1,298 parts, where sand casting tooling at about $1,500 and a $21 part price give way to die casting tooling near $22,000 and an $8.20 part price. The chart below, published by Kinetic Diecasting, compares total costs across volumes.
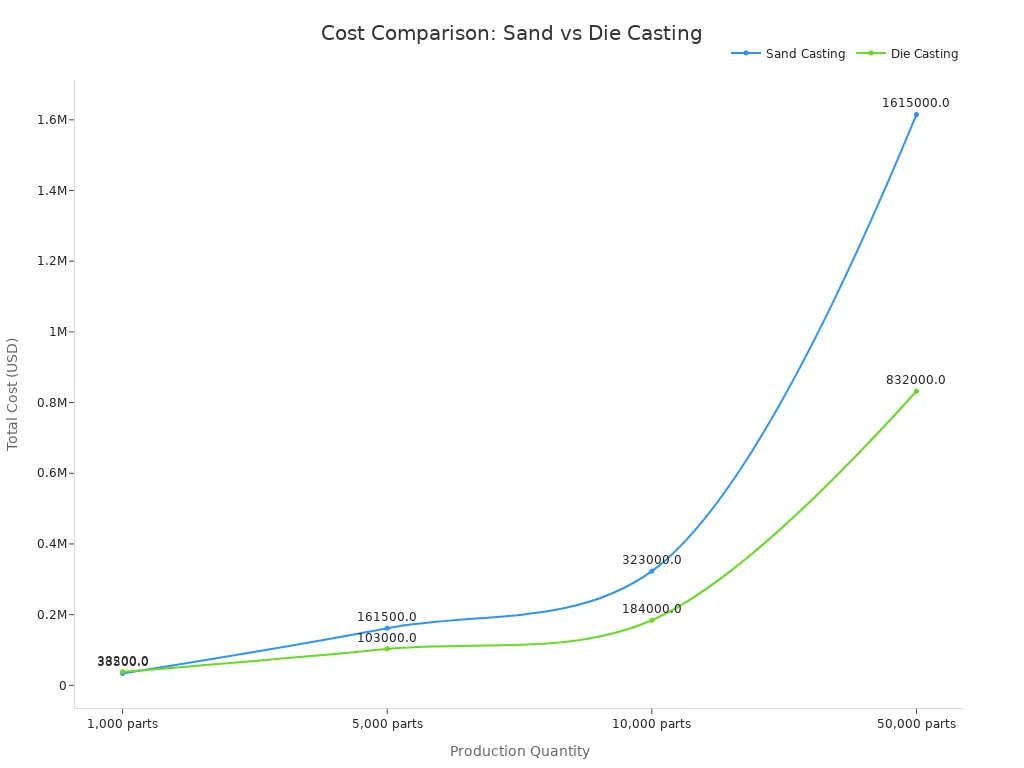
Image Source: https://www.xuxiangtaimetal.com Common Applications and Industries
Aluminum sand castings appear across a wide industrial base. Tazewell Machine works lists three major clusters.
Industry Common Applications Construction Equipment and Architectural Castings Construction machinery parts, door furniture, decorative end pieces for aluminum extrusions, decorative metal art, jobsite equipment Industrial Castings and Factory Equipment Air compressor pistons, cast blowers and impellers, explosion-proof electrical covers and boxes, heavy machinery parts, housings for industrial electronics, bearing and bushing components, valves and fittings Oil, Gas, and Energy Cast valve bodies in oil pipes, explosion-proof electrical boxes for power plants, heavy machinery for extraction, pump bodies, hydraulic equipment, power generator parts, storage tanks, turbine components Franklin Metals adds automotive engine blocks and wheels, aerospace structures, cookware, and outdoor furniture. PatSnap identifies automotive as the largest demand driver, with electrification accelerating the need for lightweight components such as battery enclosures and transmission housings.
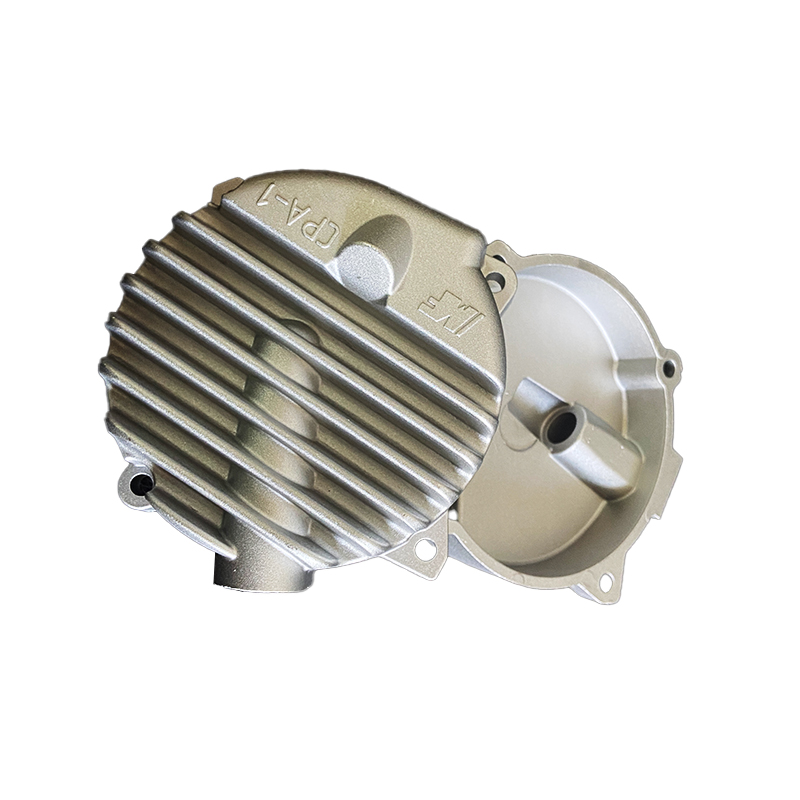
Aluminum sand casting endures because it balances design flexibility, cost, and material properties. Boose Aluminum notes that near net shape production cuts machining needs, while aluminum stays lightweight, corrosion resistant, and thermally conductive. Our foundry delivers A380 alloy components with ±0.05 mm tolerance on critical dimensions, compliant with ASTM B85/B85M and ISO 8062.
FAQ
Is aluminum sand casting cheaper than die casting?
Sand casting carries lower tooling costs. Wooden or resin patterns cost far less than steel dies. Die casting becomes cheaper at high volumes, typically above roughly 1,300 parts.
Which aluminum alloy should I choose for sand casting?
A380 offers high fluidity and good machinability for structural and fluid-handling parts. A356 provides higher strength and ductility after heat treatment. C355 suits pressure-tight applications at elevated temperatures.
What tolerances can aluminum sand casting achieve?
Standard sand casting tolerances are looser than die casting or investment casting. Critical dimensions can reach ±0.05 mm with CNC machining and inspection to ISO 8062 and ASTM B85/B85M.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.